- 1. Understanding API 5L X52 PSL1 LSAW Line Pipe Specifications and Standards
- 2. Criteria to Evaluate and Compare Line Pipes Before Procurement
- 3. Ensuring Quality and Compliance Through Inspection and Testing
- 4. Building Long-Term Partnerships with API 5L X52 PSL1 LSAW Pipe Suppliers
- 5. Conclusion
- 6. FAQ
- 7. Source Your Next LSAW Line Pipe Order with LONGMA
Sourcing high-quality API 5L X52 PSL1 LSAW line pipe begins with a clear purchase specification and a manufacturer capable of meeting it. X52 identifies a specified minimum yield strength of 360 MPa and minimum tensile strength of 460 MPa under the commonly used API 5L 46th-edition framework. PSL1 establishes product requirements, including applicable weld inspection; it is not simply a low-pressure classification. Procurement teams should confirm dimensions, service conditions, inspection and documentation before comparing offers.
Understanding API 5L X52 PSL1 LSAW Line Pipe Specifications and Standards
API 5L was updated to its 47th edition in June 2026. ISO 3183:2019 is the fourth edition and supplements API 5L, 46th edition (2018), with stated exceptions and additions. The purchase order should identify the applicable editions and any project supplements.
A complete specification lets suppliers quote the same technical scope and helps avoid changes after production. Start with the applicable edition, manufacturing route and required material properties.
The LSAW Manufacturing Process
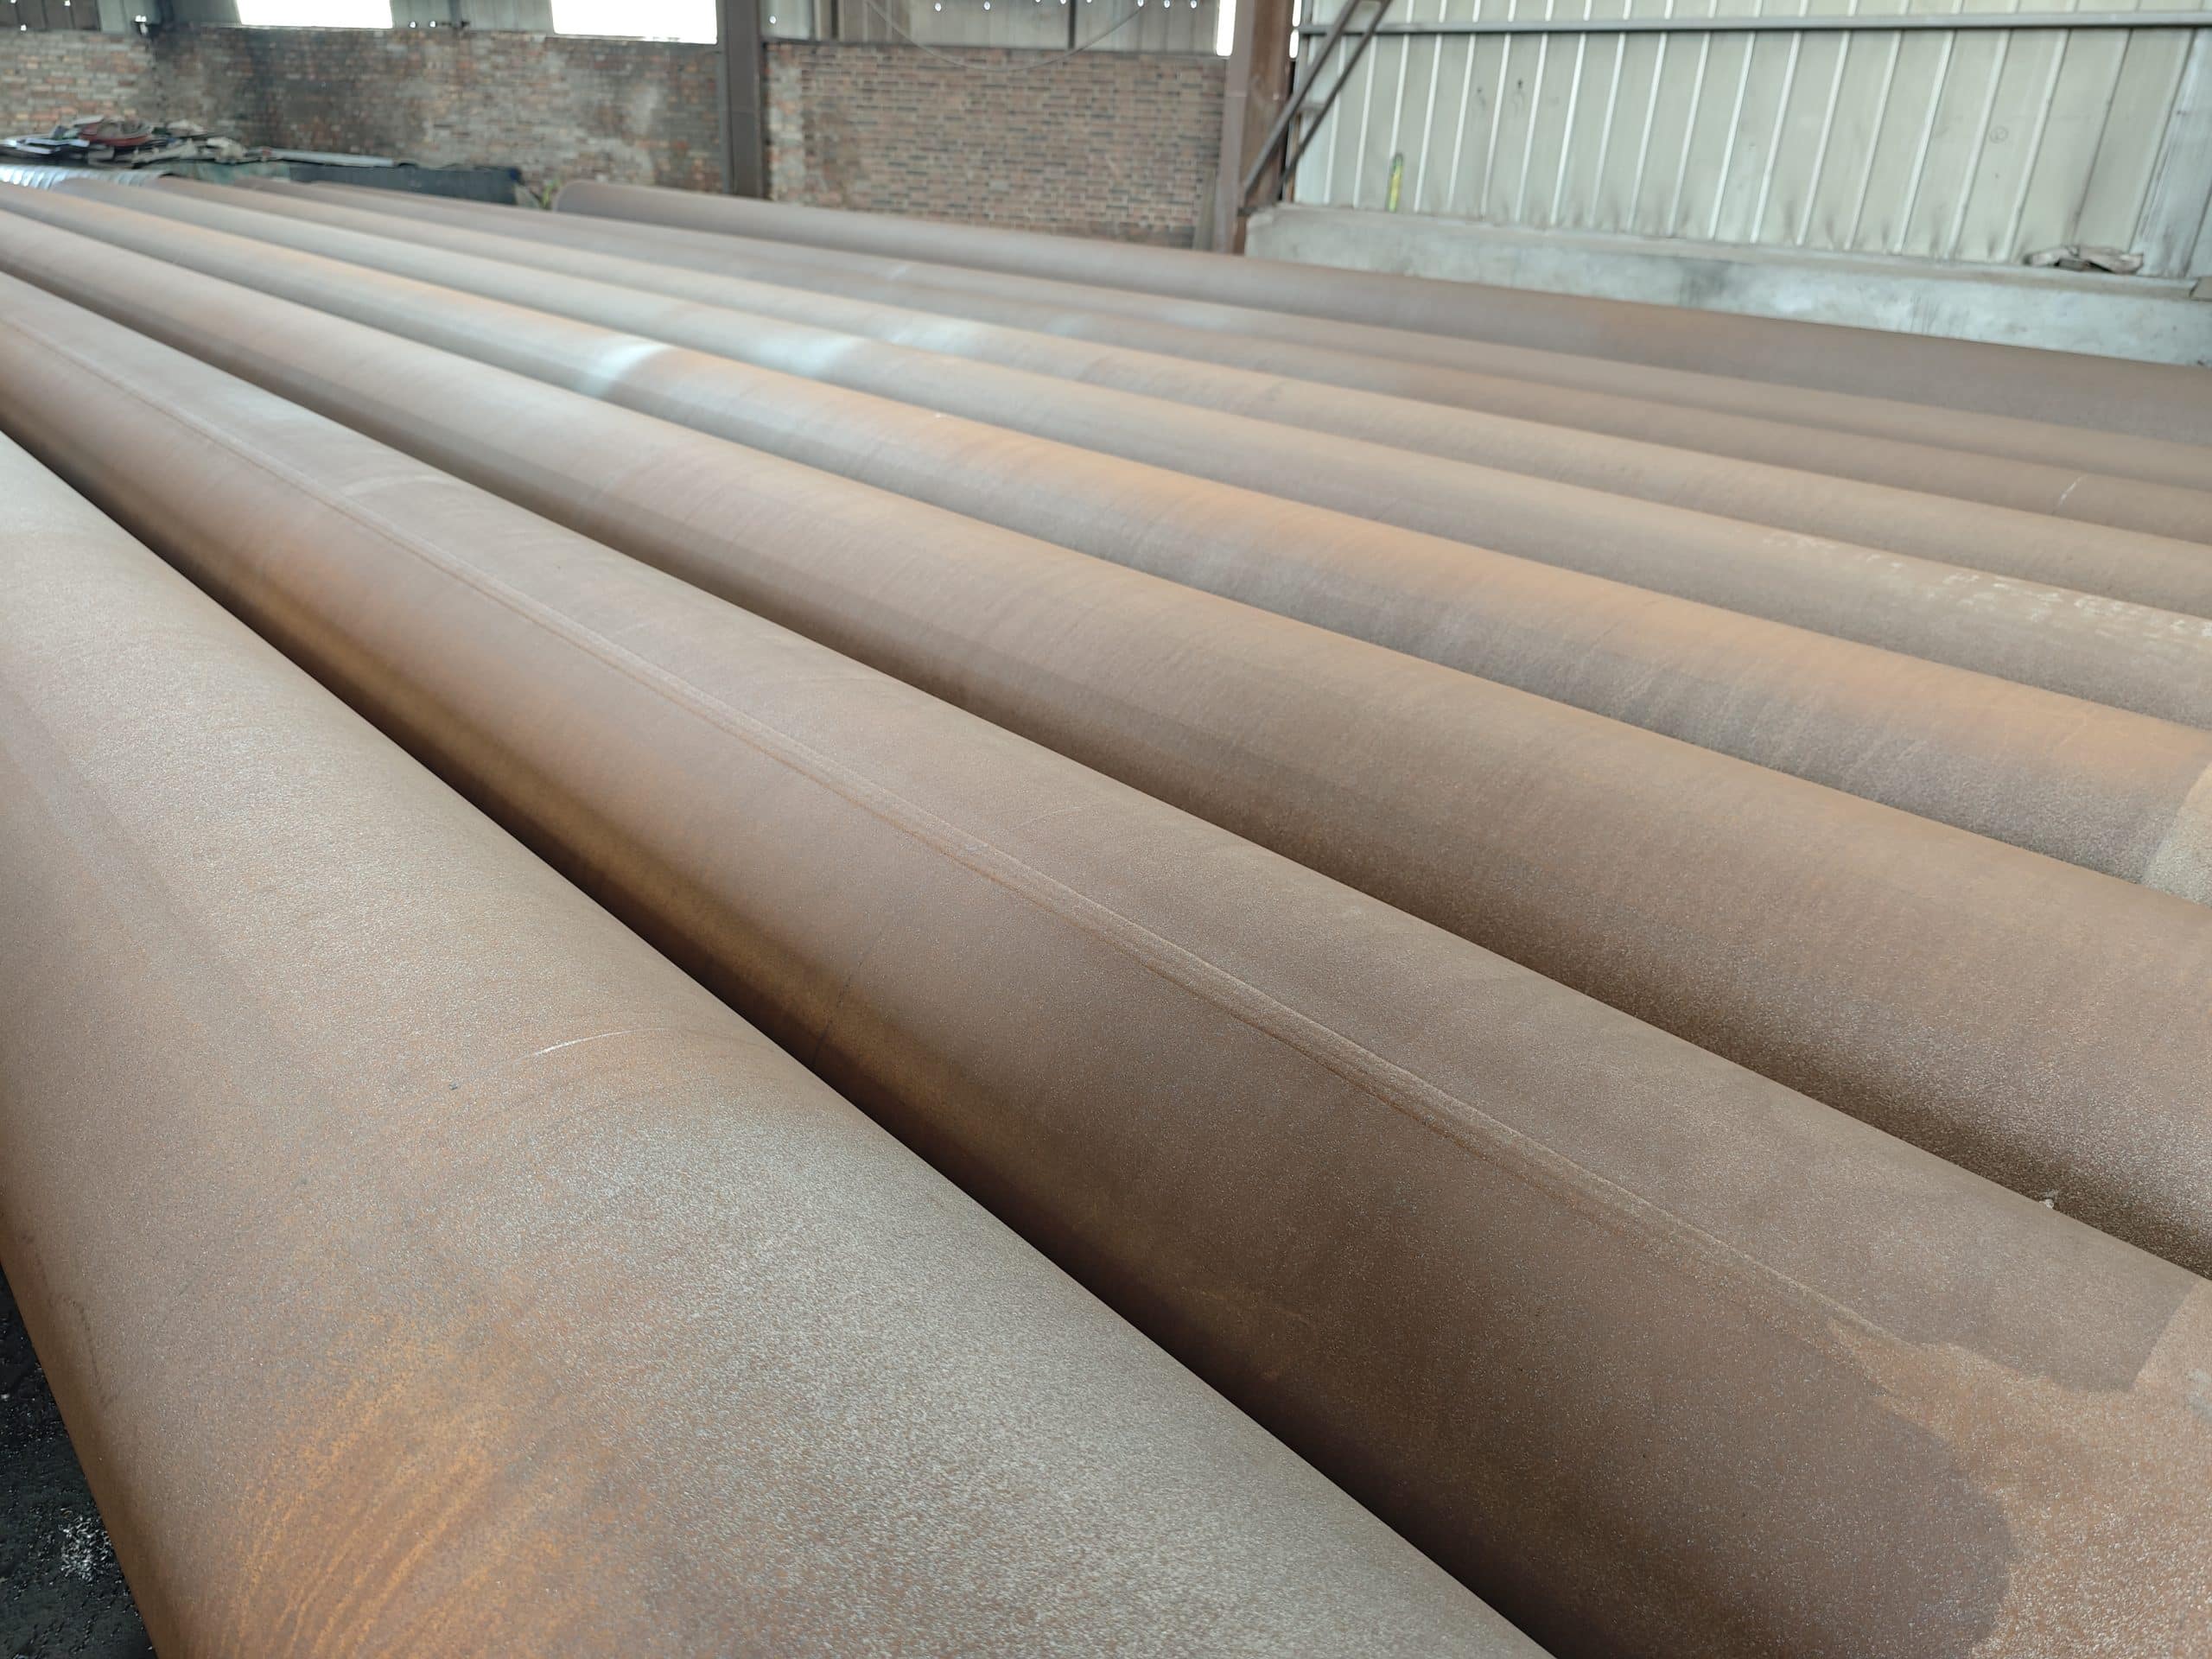
LSAW pipe is produced by forming steel plate and submerged arc welding the longitudinal seam from the inside and outside. UOE and JCOE routes include mechanical expansion, which improves dimensional control and can redistribute residual stresses without eliminating them. Available diameter, thickness and length depend on mill capability. Weld quality, hydrostatic testing and inspection must meet the ordered specification rather than an assumed generic LSAW production range.
Chemical and Mechanical Properties of X52
For X52, the specified minimum strengths are 360 MPa yield and 460 MPa tensile under the stated 46th-edition framework. The inspection certificate should report the applicable results together with the sample identity and test conditions.
Yield strength: 360 MPa minimum, with the applicable test method and acceptance criteria.
Tensile strength: 460 MPa minimum.
Carbon equivalent: identify the applicable standard or project requirement and report the selected calculation where specified; do not assume a universal 0.43 limit for all PSL1 orders.
Elongation: determine the required minimum using the applicable standard provisions and specimen dimensions, rather than treating 21% as a universal X52 value.
The design team must check these properties together with diameter, wall thickness, design factors, temperature and other loads. The steel grade alone does not establish allowable pressure or prove that X52 is more economical than another grade.
PSL1 vs. PSL2: What the Difference Means for Your Project
PSL2 adds controls on chemistry, mechanical properties, carbon equivalent and toughness, with applicable additional inspection requirements. This does not mean that every PSL2 product requires identical full-body UT. If the service is offshore or contains H₂S, supplementary requirements may apply beyond base PSL2. Specify the PSL and relevant annexes from the design basis and owner requirements rather than using a fixed pressure threshold.
Criteria to Evaluate and Compare Line Pipes Before Procurement
Choosing the right pipe grade and manufacturing route directly affects project economics and long-term pipeline integrity. The table below gives a quick comparison across the most common options:
| Attribute | X52 PSL1 LSAW | X52 PSL2 LSAW | X52 ERW | X65 PSL2 LSAW |
| Minimum yield MPa | 360 | 360 | 360 | 450 |
| PSL | PSL1 | PSL2 | Specify PSL | PSL2 |
| Toughness | Project additions as ordered | Applicable PSL2 requirements | Depends on PSL and order | Applicable PSL2 requirements |
| Weld NDT | Required as applicable | Required as applicable | Required as applicable | Required as applicable |
| Sour service | Not established by base PSL1 | Additional qualification | Additional qualification | Additional qualification |
Matching Grade to Operating Conditions
Select grade, wall thickness and PSL using the governing design code and service conditions. Neither 10 MPa nor 12 MPa is a universal boundary between PSL1 and PSL2. H₂S assessment must consider water, partial pressure, pH, temperature, stress and the scope of the applicable material-selection standard. A single H₂S partial-pressure value is not a complete selection rule. Where API 5L Annex H is specified, order its corresponding PSL2 sour-service requirements.
Corrosion Resistance and Coating Selection
Buried or submerged carbon-steel pipelines require a project-specific corrosion-protection strategy. FBE, 3LPE and 3LPP are common coating options, with temperature and installation limits assessed separately. Specify the correct application standard and edition for each system. Typical FBE thicknesses may fall around 400–600 µm, but the project specification governs. Coating, cathodic protection, field-joint treatment and repairs should be considered together; a polyethylene jacket does not replace the complete corrosion-control design.
Total Cost of Ownership vs. Initial Unit Price
A lower unit price on pipe with poor dimensional control can increase field welding time and reject rates, which is often far more expensive than the price saving. Request mill dimensional inspection data—specifically ovality and straightness records—alongside the mill test certificate (MTC) to benchmark suppliers on quality, not just price.
Ensuring Quality and Compliance Through Inspection and Testing
No amount of documentation replaces physical verification. A sound inspection plan covers three stages: incoming material, in-process, and final release.
Non-Destructive Examination Requirements
API 5L provides NDT requirements for SAW pipe, including PSL1 weld inspection. Required methods, coverage and any complementary examinations must be established from the ordered edition, manufacturing route and relevant annexes. Distinguish weld NDT, pipe-end lamination examination and pipe-body inspection. A blanket statement that PSL2 always requires full-body UT is insufficient. The approved inspection plan should identify acceptance criteria and the records required for release.
Mechanical and Chemical Testing Traceability
Maintain traceability from each finished pipe to its steel-plate heat and applicable production records. The MTC should include the ordered chemical analysis, tensile properties and elongation, with carbon-equivalent reporting where specified. LONGMA uses heat, batch and product identification to connect material, inspection and finished-pipe records. Check that markings and documentation remain consistent after coating and shipment preparation.
Third-Party Source Inspection
For projects where Saudi Aramco, ADNOC or comparable national oil company standards apply, source inspections are frequently carried out at the mill by owner-appointed inspectors. A suitable inspection strategy, calibrated equipment and specific hold points must be in place at the mill. Before making the purchase, not after, confirm with the supplier that they allow and consistently host third-party inspectors.
Building Long-Term Partnerships with API 5L X52 PSL1 LSAW Pipe Suppliers
Consistent performance over repeat orders can reduce qualification work, provided the approved manufacturing scope and project requirements remain comparable. Review previous delivery performance alongside current technical capability.
Assessing Supplier Track Record
Ask for relevant project experience, including product specifications, dimensions and inspection scope. LONGMA has supplied projects involving SINOPEC, CNPC, PEMEX, PDVSA and PTTEP. Customer information may be subject to confidentiality, so assess available references alongside audit findings and inspection records rather than treating disclosure of client names as the sole qualification test.
Negotiating Framework Agreements and SLAs
For customers that purchase a lot of the same product every year a framework supply agreement that locks in pricing formulae (e.g. basic steel price index plus a set fabrication premium), minimum stock requirements, and maximum lead-time commitments is excellent for everyone. The SLA should contain inspection hold points, response timings for non-conformances and wait periods for replacement pipes to keep your project on pace.
Conclusion
Quality sourcing requires comparable technical offers, verified manufacturing capability and an inspection plan that can be implemented before shipment. State the standard edition, dimensions, grade, PSL, service conditions, coating and certificate type in the RFQ. Confirm hold points and traceability before production. These steps help control procurement risk while allowing suppliers to price the actual scope rather than an incomplete description.
FAQ
What does PSL1 mean for X52 LSAW pipe?
PSL1 is a product specification level with requirements for chemistry, mechanical properties, hydrostatic testing and applicable weld NDT. It does not impose the same general toughness requirements as PSL2. Suitability still depends on the design and service specification.
What is the minimum yield strength of API 5L X52?
Under the stated API 5L 46th-edition framework, X52 has a specified minimum yield strength of 360 MPa and minimum tensile strength of 460 MPa. Confirm the exact product requirements in the edition specified by the contract.
Can X52 PSL1 LSAW pipe be used in sour service?
Ordinary PSL1 certification alone does not establish sour-service suitability. Adding an S suffix to a PSL1 designation is not a substitute for qualification. Where API 5L Annex H applies, specify the corresponding PSL2 grade, supplementary tests and environmental requirements.
What sizes does LONGMA supply for LSAW pipe?
LONGMA manufactures round ERW and LSAW steel pipes. Confirm the LSAW-specific outside diameter, wall thickness and length in the quotation instead of applying the company’s combined ERW and LSAW range to one process. Specify thickness directly or pair a schedule designation with nominal size and dimensional standard.
How long does delivery take?
Stocked sizes may ship in as little as 7 days. Special grades and sizes are usually available in 30 days. Custom parameters will take roughly 45 days from the time of purchase confirmation.
Source Your Next LSAW Line Pipe Order with LONGMA
LONGMA has manufactured steel line pipe since 2003. Our factory covers 230,000 m², with annual output exceeding 500,000 tonnes and more than 60 senior technical personnel. We support X52 PSL1 LSAW orders with traceable inspection records, EN 10204 documentation and agreed third-party inspection. Other grades and PSLs are quoted separately according to manufacturing capability. Contact info@ilongma.com or visit www.ilongma.com for a technical review and quotation.